HRDC Claimable Training
7 structured modules. One stronger moulding organisation.
Build capability • Improve consistency • Strengthen technical decision-making

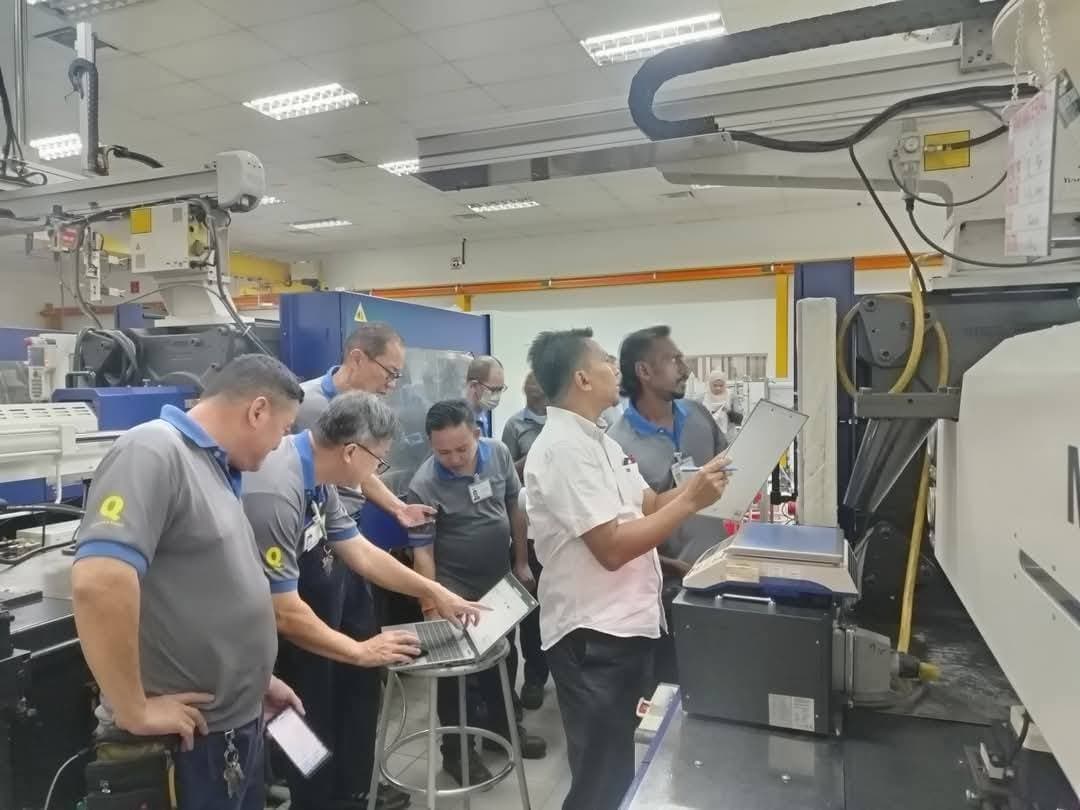
About the Trainer

Move from memorized settings to scientific material-and-process thinking
Build Engineers Who understand The Process.
A two-day foundation linking material, mould, machine and process to safer, clearer and more consistent workplace performance.
By Ts. Mohd Hafiedzzul Bin Malek Riduan — 17+ years, HRD Corp Accredited
new engineers learn isolated tasks without the complete process.
numbers are repeated without understanding the plastic.
production concerns are interpreted without evidence.
symptoms, mechanisms and possible causes are confused.
production, quality and tooling lack a shared language.
the same fundamentals must be explained repeatedly.
A DEFECT IS A SYMPTOM — NOT AUTOMATIC PROOF OF ITS ROOT CAUSE. Fundamentals help engineers observe accurately, communicate clearly and avoid unsupported assumptions.
Establish one consistent foundation for every new engineer.
Replace unsupported assumptions with structured observation.
Improve recognition and communication of part abnormalities.
Align engineering, production, quality and tooling.
Prepare the workforce for future scientific development.
Connect material, mould, machine and process.
Explain temperature, flow, pressure and cooling.
Separate observations, physical mechanisms and possible causes.
Use accurate terminology and approved standards.
Build readiness for supervised scientific development.
Thermoplastic behaviour, moisture awareness, viscosity and thermal response. Understand what the plastic requires.
Cavity, core, runner, gate, cooling, venting and ejection functions. Recognise how tooling shapes part quality.
Main components, general functions, process delivery and safety boundaries. Connect equipment capability with the process.
Filling, packing, cooling, plasticising and observable quality evidence. Explain basic cause-and-effect across the cycle.
Format: Guided discussions, Prepared samples, Process diagrams, Case studies, Participant worksheets
A TWO-DAY TRAINING - HRDC Claimable
UNDERSTAND THE MATERIAL & CONTROL THE RESULTS.
Develop engineers who explain resin behaviour, material condition and production variation before recommending evidence-based scientific molding decisions.
By Ts. Mohd Hafiedzzul Bin Malek Riduan — 17+ years, HRD Corp Accredited
Different resin grades are treated as if they behave identically.
Temporary adjustments hide the actual material-related mechanism.
Drying condition and moisture sensitivity are poorly understood.
Material documents and batch differences are not investigated.
Cooling and material response are judged by habit, not evidence.
Critical technical decisions depend on a few experienced people.
BETTER MATERIAL UNDERSTANDING CREATES BETTER DECISIONS. Review outcomes through scrap, rework, investigation time, lot variation, cycle stability and knowledge transfer.
Address preventable variation and protect the cost of quality.
Use material evidence to identify likely causes more quickly.
Improve alignment across resin lots, production shifts and teams.
Evaluate cycle and cooling assumptions with technical reasoning.
Reduce dependency on individual experts and retain knowledge.
A structured connection between resin behaviour and process intent.
A clearer approach to TDS, COA and material-sensitive variation.
Consistent communication across production, quality and engineering.
Relate polymer family and structure to flow behaviour, thermal sensitivity, shrinkage and cooling response.
Use material identity, supplier information and resin behaviour to explain an evidence-based processing intent.
Connect recurring symptoms with plausible moisture, thermal-history, resin or wider 4M mechanisms.
Distinguish hygroscopic and non-hygroscopic materials and understand why material condition matters.
Interpret document purpose, material recommendations and lot information before technical conclusions.
Grade, lot and condition
Flow, thermal response, shrinkage
Temperature | Flow | Pressure | Cooling
Method, mold and machine interaction
Evidence and acceptable quality
Machine settings are control inputs, not proof. The materials perspective checks the interaction of Material, Method, Mold and Machine.
Different polymers are treated the same.
Explain polymer structure, flow, thermal response and shrinkage.
Production decisions are based on copied assumptions.
Connect material behaviour with the four plastic conditions.
Moisture-sensitive symptoms keep returning.
Understand resin sensitivity and material-condition risks.
Supplier and batch information is overlooked.
Use material documents as evidence in technical decisions.
Different thermoplastics are processed using the same assumptions.
Connect material family, molecular structure, flow behaviour, shrinkage and cooling response.
Decisions rely on copied settings instead of material evidence.
Relate rheology and thermal behaviour to temperature, flow, pressure and cooling.
Material-sensitive defects and degradation are misunderstood.
Recognise drying-related risks and distinguish material mechanisms from other 4M causes.
TDS, COA and SDS information is collected but not applied correctly.
Interpret material identity, recommended ranges, lot variation and document purpose.
For: Process engineers and technicians, QA/QC personnel, Production supervisors, Material handlers, Setup technicians, Technical managersFormat: Guided discussion, Prepared defect case studies, Material-data interpretation, Cross-functional 4M thinking
Build the essential principles behind structured process development
A two-day bridge from the fundamentals to structured development work, built on the four plastic conditions and a shared definition of repeatability.
By Ts. Mohd Hafiedzzul Bin Malek Riduan — 17+ years, HRD Corp Accredited
the process is set up differently each time, depending on who is on shift.
filling, packing and cooling are adjusted together without separating their roles.
values are written down, but actual process outputs are not read.
teams do not agree on what repeatable means.
numbers are gathered without a clear purpose.
the basics are missing, so advanced development training is hard to absorb.
| BEFORE | AFTER |
|---|---|
| Adjust settings until parts look acceptable | Follow a phase-by-phase development logic |
| Record setpoints only | Read actual outputs alongside setpoints |
| "Stable" means "it ran well today" | Repeatability has a shared meaning and indicators |
replace random adjustment with a clear development sequence.
connect each process phase to what the plastic experiences.
turn recorded values into usable evidence.
align engineering, production and quality.
prepare the team for 4-day Process Development.
Name each phase and state its purpose.
Distinguish what is set from what the process actually does.
Turn recorded figures into a statement about the process.
State the definition and the signs that support it.
Document so another engineer can follow it.
Understand the structure
Apply the basics
For: Process engineers and technicians, Setup technicians, Production supervisors, QA/QC personnelFormat: Guided discussions, Process diagrams, Prepared data sets, Case studies, Participant worksheets
FOUR-DAY PROFESSIONAL TRAINING FOR ENGINEERING TEAMS
STOP GUESSING. START DEVELOPING WITH EVIDENCE.
Develop engineers who can evaluate process evidence, explain variation and support more stable, repeatable injection-moulding production.
By Ts. Mohd Hafiedzzul Bin Malek Riduan — 17+ years, HRD Corp Accredited
Settings are changed without understanding the actual process response.
Scrap and rework continue when symptoms receive only temporary fixes.
Different personnel obtain different results from the same mould.
Unstructured development prolongs start-up and recovery time.
Machine settings are recorded, but actual outputs are not understood.
Critical process knowledge stays with one experienced individual.
Improve understanding of recurring defects, scrap, rework and process variation.
Replace repeated trial-and-error with an organised, evidence-based development approach.
Improve communication and process consistency across shifts, personnel and production runs.
Document approved process information and reduce reliance on a few experienced individuals.
Use machine, material and mould evidence to explain decisions to management and customers.
Evaluate readiness, process behavior, repeatability and approved documentation systematically.
Connect temperature, flow, pressure and cooling with what the plastic actually experiences.
Review fill time, pressure response, cushion, part weight and cavity-to-cavity variation.
Distinguish the defect, physical mechanism and possible material, mould, machine or method causes.
Communicate approved process information clearly across engineering, production and quality.
Actual delivery and speed-linearity evidence.
Flow behaviour and rheology evidence.
Cavity balance, filling response and variation.
UNDERSTAND
DEVELOP
EVALUATE
SUSTAIN
For: Process engineers, Engineering managers, Production supervisors, Quality engineers, Technical specialists
Introduce a consistent framework for parameter-setting decisions
A two-day bridge from personal habit to shared engineering capability, using plastic conditions, evidence and controlled decisions.
By Ts. Mohd Hafiedzzul Bin Malek Riduan — 17+ years, HRD Corp Accredited
the same mould is set up differently on every shift.
parameters are changed with no stated intent.
the team cannot tell which action worked.
setting discussions jump randomly between parameters.
values from a similar job are reused without checking the conditions.
the next person inherits numbers but not the logic.
| BEFORE | AFTER |
|---|---|
| Change several parameters and hope | Change one thing at a time with a stated intent |
| Copy the last setup | Decide settings from plastic conditions and evidence |
| Numbers handed over without reasons | Rationale recorded for the next person |
one method across shifts and personnel.
production, quality and engineering use the same logic.
every change has an intent and a recorded response.
decisions can be followed and reviewed.
the method belongs to the team, not one person.
Connect each group to Temperature, Flow, Pressure and Cooling.
Use an agreed sequence rather than personal habit.
State why a change is being considered.
Change one thing at a time and document what happened.
Make the reasoning available to the wider team.
Parameter logic
Structured method in practice
For: Process engineers and technicians, Setup technicians, Production supervisors, Technical managersFormat: Guided discussions, Prepared case studies, Decision worksheets, Process diagrams, Group review
2 DAYS ENGINEER-FOCUSED IN-HOUSE 9:00 AM - 5:00 PM Evidence and case studies Tailored to client needs
When defects become business problems
The same defect returns after a temporary setting adjustment. Several parameters are changed together and the team cannot explain which action worked. Troubleshooting depends on senior staff instead of a repeatable company method. Machine, Mold, Material and Method causes are confused or investigated randomly. Production, quality and tooling disagree because decisions are not supported by common evidence. Corrective actions are not validated documented or converted into prevention standards.
By Ts. Mohd Hafiedzzul Bin Malek Riduan — 17+ years, HRD Corp Accredited
Turn defect troubleshooting from an individual skill into a shared, evidence-based engineering capability.
Lower scrap, rejection and rework by replacing temporary fixes with better-supported corrective actions.
Faster production recovery through a structured investigation that reduces random trials.
More consistent decisions across shifts using one shared troubleshooting language and method.
Less dependence on a few senior employees by strengthening the engineering team's first-response capability.
Stronger prevention and knowledge retention through validated actions, records and lessons learned.
Differentiate similar-looking visual, dimensional and material defects before selecting an investigation path.
Connect the symptom with plastic temperature, flow, pressure, cooling and material behaviour.
Interpret defect pattern, cavity, frequency, process outputs and the last known good condition.
Separate Machine, Mold, Material and Method hypotheses using relevant supporting evidence.
Document the reasoning, validate repeatability and recommend recurrence-prevention actions.
Actual delivery
Cavity condition
Material behaviour
Approved process
DIAGNOSE CORRECTLY
VERIFY AND PREVENT
Short shot, flash, burn marks, sink marks, jetting, gate blush, flow lines and weld lines.
Oversized or undersized parts, warpage and deformation.
Splay, bubbles, brittleness, cracking, contamination and inconsistent colour.
For: Process engineers, technicians, supervisors, quality personnel, engineering managersFormat: Prepared defect samples, production data, 4M worksheets, group case studies
Complete Professional Training Portfolio
Build capability - Improve consistency - Strengthen technical decision-making
By Ts. Mohd Hafiedzzul Bin Malek Riduan — 17+ years, HRD Corp Accredited
Seven modules. Clear outcomes. Practical value.
Develop a shared, evidence-led understanding of scientific moulding.
Create a common technical foundation across the organisation.
Understand how thermoplastic behaviour influences moulding quality.
Connect material characteristics to product and process performance.
Build the essential principles behind structured process development.
Prepare the team for more advanced process-development learning.
Advance towards more robust, consistent process-development thinking.
Strengthen the ability to evaluate and standardise process decisions.
Introduce a consistent framework for parameter-setting decisions.
Promote a logical, shared approach to process-setting discussions.
Explore a structured, evidence-led approach to recurring defects.
Improve problem identification and the quality of defect investigation.
Understand how a defined process can remain consistent across contexts.
Support reproducibility and communication across teams or locations.
Start with the right foundation, then progress according to participant readiness.
Develop a common technical language and a more confident engineering team.
Strengthen evidence-led decisions, process discipline and learning continuity.
Select the modules that match business needs and participant readiness.
WHY SCIENTIFIC MOULDING
Four recurring problems we see across Malaysian injection moulding operations. Four shifts that scientific thinking delivers.
Four recurring problems
Numbers are repeated without understanding the plastic. Different resin grades treated as if they behave identically.
Temporary adjustments hide the actual mechanism. Same defect returns after a setting change.
Critical decisions depend on a few senior experts. Knowledge stays with individuals, not the team.
Machine settings are recorded, but actual outputs are not understood. Decisions rely on habit, not evidence.
Four shifts scientific thinking delivers
Understand what the plastic requires, then set the machine.
Symptom, mechanism and cause separated. Corrective actions validated and documented.
One troubleshooting language. First-response capability built across shifts.
Process behaviour explained by evidence. Approved conditions documented for the team.
TRACK RECORD
Seventeen years building scientific moulding capability. Hundreds of engineers trained. Dozens of manufacturing partners.
HRD Corp Accredited Trainer
Training programmes are HRDC-claimable for Malaysian employers.
Ts. Mohd Hafiedzzul Bin Malek Riduan
The same trainer who wrote the programmes delivers them. No subcontracting, no junior facilitator. Direct from practitioner to team.
Trainer track record: seventeen years, five hundred personnel trained, sixty Malaysian manufacturing companies
TESTIMONIALS
Feedback from engineers and managers who have completed the programmes.
Participant testimonials from the Scientific Moulding training programmes
REQUEST A PROPOSAL
Tell us about your team and training needs. We'll send a customised in-house proposal within 2 working days.
Phone
+60 12-488 5247Replies within 2 working days